Choosing the China Best Brass Cast Manufacturer for Global Buyers requires more than comparing prices. Brass Cast quality depends on alloy control, mold design, pouring temperature, machining accuracy, and inspection discipline. A polished website cannot prove any of these capabilities.
John Campbell, a respected casting researcher and author, said, “Castings are not made; they are grown.” This principle matters on the factory floor. Skilled technicians monitor furnace readings, remove surface defects, and inspect threaded holes under bright inspection lights. Reliable manufacturers can provide material certificates, dimensional reports, sample approvals, and traceable production records. They should also explain which brass grades suit plumbing parts, valves, decorative hardware, or industrial components.
Global buyers should examine equipment, process consistency, communication, packaging, and export experience together. A serious supplier welcomes video audits and accepts third-party inspections. It also discusses tolerances before production begins. No manufacturer is perfect. Even a strong Brass Cast supplier may face porosity, color variation, or delayed tooling during complex projects. That weakness should be acknowledged, not hidden. Buyers need clear corrective actions, realistic lead times, and documented quality controls. The best partnership grows through evidence, not promises. This guide evaluates Chinese Brass Cast manufacturers through practical criteria, technical knowledge, and buyer-focused verification.
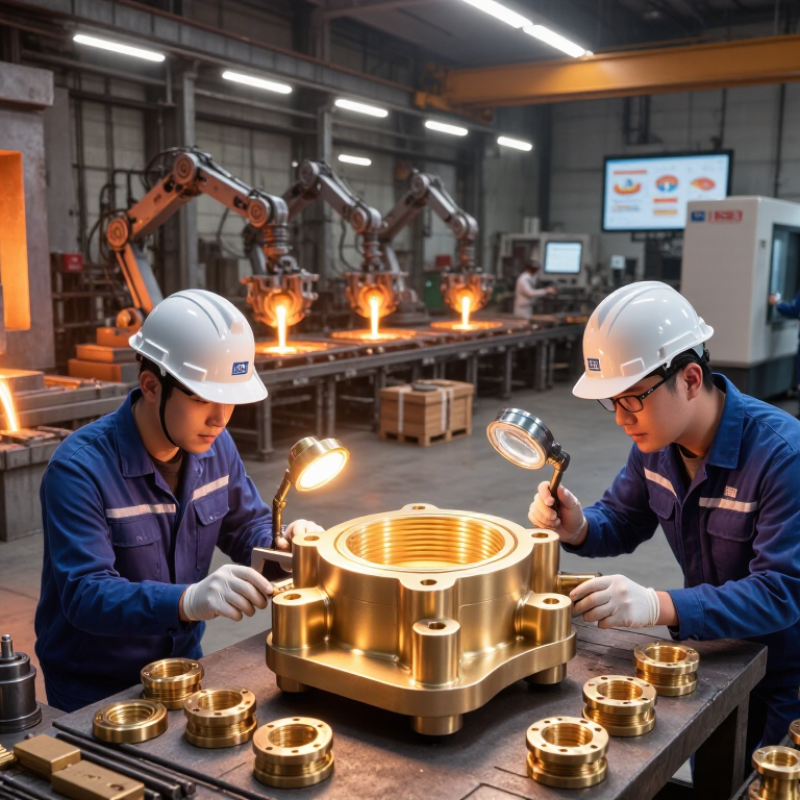
China’s brass casting industry serves buyers seeking stable copper-zinc components for valves, fittings, hardware, and industrial assemblies. A brass alloy containing 55–65% copper usually contains 35–45% zinc, with small additions controlling strength, machinability, or casting behavior. The balance is zinc.
Copper generally improves ductility, corrosion resistance, and thermal conductivity. Zinc can improve fluidity and reduce material cost. However, more zinc does not automatically create a better casting. It may increase brittleness or produce inconsistent color when the chemistry shifts. Small chemistry changes matter. Experienced foundries verify melt composition before pouring, rather than trusting visual appearance.
Casting method also affects the result. Sand casting suits larger shapes and lower production volumes. Gravity die casting can provide cleaner surfaces and repeated dimensions. Pressure casting supports thin walls, but trapped gas and porosity require careful control. Buyers should request alloy chemistry, dimensional reports, surface inspection, and sample approval. A practical inspection checks threads, edges, wall thickness, and leakage under pressure. Surface finish can mislead. A bright component may still contain internal defects. My own preference is to review process records alongside samples, because one attractive part cannot prove stable production. Even well-controlled brass casting can need adjustment after the first production run.
| Representative Alloy / Family | Copper Content (wt. %) | Typical Additional Elements (wt. %, balance mainly zinc) | Casting Characteristics | Typical Applications | Important Production Considerations |
|---|---|---|---|---|---|
| High-strength yellow brass UNS C85200–C85800 family | Approximately 60–68 | Lead commonly up to about 3; iron and manganese are often added for strength; exact limits vary by grade. | Good strength and wear resistance; suitable for sand casting and other approved copper-alloy casting methods. | Valve bodies, pump components, marine hardware, brackets and general engineering castings. | Control pouring temperature and mold filling to reduce misruns, shrinkage and gas-related defects. Confirm lead limits when drinking-water contact is involved. |
| Manganese bronze UNS C86300 | 60–66 | Aluminum about 5–7.5; manganese about 2.5–5; iron about 2–4; zinc is the balance. | High strength, hardness and abrasion resistance; generally more demanding to machine than leaded yellow brass. | Heavy-duty gears, bushings, wear plates, valve parts and marine components. | Requires accurate alloy control and effective feeding because the alloy can develop shrinkage defects. Heat treatment and cooling practice affect final properties. |
| Manganese bronze UNS C86500 | 60–66 | Aluminum about 5–7; manganese about 2–4; iron may be present at approximately 2–4; zinc is the balance. | Strong cast alloy with good resistance to impact and sliding wear; often selected for robust industrial castings. | Bearings, gears, heavy-duty bushings, valve components and structural machine parts. | Use clean charge materials and protect the melt from excessive oxidation. Dimensional control is important because complex castings may distort during cooling. |
| Silicon yellow brass UNS C87500 family | Approximately 58–64 | Silicon commonly about 2–4; manganese and iron may be added in controlled amounts; zinc is the balance. | Good castability and strength; silicon can improve fluidity and contributes to wear and corrosion performance. | Plumbing components, valve bodies, pump parts, fittings and engineering castings. | Avoid uncontrolled silicon or iron additions because they can change fluidity, hardness and machinability. Welding and repair procedures require alloy-specific qualification. |
| Leaded silicon brass UNS C87850 family | Approximately 62–64 | Silicon about 2.5–4; lead is controlled for machinability; zinc is the balance. | Good fluidity and machinability, making it suitable for detailed castings that require subsequent drilling, tapping or turning. | Industrial fittings, meter components, valve parts and precision-machined castings. | Lead content must be checked against the destination market and service conditions. Use dedicated machining and waste-handling controls where required. |
| General cast yellow brass 55–65% copper range | 55–65 | Zinc is typically the largest remaining element; lead, iron, manganese, aluminum or silicon may be added according to the specified grade. | The copper-to-zinc ratio strongly affects color, strength, ductility, fluidity and corrosion behavior. Exact alloy designation is essential for repeatable results. | Hardware, fittings, decorative parts, mechanical components and general-purpose cast products. | Do not purchase by copper percentage alone. Specify the applicable UNS grade, chemical limits, casting process, mechanical requirements, inspection method and surface finish. |
China Best Brass Cast Manufacturer for Global Buyers?
Key Casting Grade: CuZn39Pb3 Contains 57–59% Copper under EN 1982
For global buyers, choosing a brass casting manufacturer begins with material discipline, not attractive photographs. CuZn39Pb3 suits threaded bodies, valve parts, adapters, and small precision castings. Under EN 1982, its stated copper range is 57–59%, while zinc forms most of the balance. Lead improves machinability and supports efficient turning after casting. That lead content matters. Buyers should confirm the intended service and applicable market requirements before approving production.
An experienced foundry should control charge materials, melting temperature, mould filling, and cooling conditions. Each heat needs traceable records, including batch identity, chemical analysis, and casting date. Practical inspection may include spectrometer testing, dimensional checks, surface examination, and pressure testing for fluid-carrying parts. Ask for sample sections. A polished surface can hide shrinkage or porosity. It happens.
For overseas projects, drawings should state EN 1982, alloy designation, tolerances, machining allowance, and acceptance criteria. The supplier should explain whether parts use sand casting, gravity die casting, or pressure casting. Each method affects detail, cost, and defect risk. Packaging also deserves attention; separators and dry protection reduce impact marks and oxidation during transit. No factory gets every variable right. A reliable manufacturer admits process limits, investigates rejected samples, and adjusts tooling with evidence. That attitude often matters more than a low initial quotation.
Choosing the best brass cast manufacturer for global buyers requires more than comparing prices.
Quality begins with proven control over melting, mold preparation, machining, and inspection. ASTM B584 covers copper-alloy sand castings, including chemical composition and mechanical requirements for suitable applications. EN 1982 provides another important benchmark for copper and copper-alloy castings used in international projects.
ISO 9001 compliance strengthens the manufacturing system behind the casting. It supports controlled procedures, employee training, corrective actions, and traceable inspection records. A reliable supplier should provide material certificates, heat numbers, dimensional reports, and test results when requested.
Pressure testing may also be necessary for valves, fittings, and fluid-handling parts. Standards help, but they do not replace practical experience. Small issues, such as uneven wall thickness or unclear drawings, can still create expensive failures.
Tips: Ask whether the supplier can match the required ASTM or EN grade before production. Confirm sampling methods and acceptance criteria in writing. Review recent inspection records, not only a certificate. If possible, inspect the casting surface and section quality during a pre-shipment check. No process is perfect. Even experienced teams should review defects, question assumptions, and improve controls after every production batch.
A reliable brass casting manufacturer should prove control, not merely promise quality. During factory evaluations, I compare approved drawings with actual parts, batch records, and inspection reports. Critical dimensions need calibrated gauges, not visual judgment. Bore diameter, thread depth, and sealing surfaces deserve special attention. Small deviations can cause large assembly problems. Ask for the stated tolerance on every key feature. A vague tolerance is a warning sign.
Pressure testing must match the component’s working conditions. The factory should define test pressure, holding time, medium, and acceptance criteria before production. For pressure-bearing castings, 100% testing is more convincing than occasional sampling. Inspectors should record serial numbers, test results, and rejected pieces. Look for wet areas around plugs or joints. They often reveal leakage before shipment. Test equipment also needs calibration records.
A good supplier combines process control with final inspection. Inspectors should check casting surfaces, porosity, threads, dimensions, and packaging. Photos help, but they do not replace physical records. I once accepted a report that looked complete, yet its gauge calibration had expired. That mistake was avoidable. No factory is flawless. The important question is whether problems are reported, corrected, and prevented from returning. Independent pre-shipment inspection can add useful confidence for global buyers.
Choosing a brass cast manufacturer for global buyers requires more than comparing unit prices. Export readiness starts with documented quality controls. IATF 16949 supports disciplined process management, risk analysis, corrective action, and measurement. In practice, this means checking furnace temperatures, mold conditions, machining dimensions, and inspection results. A supplier should provide current certificates and explain their scope clearly. Paperwork alone is not proof.
RoHS and REACH compliance requires controlled material selection and reliable declarations. Buyers should request alloy composition reports, restricted-substance test results, and updated compliance statements. These documents should match the actual brass grade supplied. A traceable batch record should connect the casting lot, furnace charge, operator, inspection data, and shipping documents. Records matter. If one link is missing, investigating a field issue becomes slower and more expensive.
Experienced exporters also verify packaging, labeling, dimensional reports, and commercial documents before shipment. A lot number stamped on a box is useful only when the factory can retrieve its production history. During audits, buyers should inspect real records, not only sample templates. No system is flawless. A small labeling error or delayed test report can still occur, so capable manufacturers need clear escalation procedures and documented corrections. This practical transparency often shows more reliability than polished promises.
The chart compares the publication years of the key frameworks commonly used to evaluate automotive quality, restricted substances, chemical compliance, and product traceability. IATF 16949:2016 supports automotive quality management, RoHS Directive 2011/65/EU addresses restricted substances in electrical and electronic equipment, REACH Regulation (EC) No 1907/2006 governs chemicals in the EU, and ISO 9001:2015 includes identification and traceability controls.
References: IATF 16949:2016; RoHS Directive 2011/65/EU and Delegated Directive (EU) 2015/863; REACH Regulation (EC) No 1907/2006; ISO 9001:2015.
Stay in touch with the latest National Luna Products and News!